

Scrap rates in high-tolerance discrete manufacturing remain a persistent drag on operating margins, eating directly into EBITDA while plant managers rely on tribal knowledge and manual adjustments to keep lines running. When tolerances tighten to the micron level, even minor variations in raw material hardness or ambient shop temperature can push a production run out of spec, resulting in expensive rework or total scrap. Traditional trial-and-error tuning hits a wall because human operators cannot simultaneously analyze multivariate sensor feeds, historical tool wear data, and real-time CNC telemetry fast enough to prevent dimensional drift. Implementing algorithmic parameter tuning scrap rates offers a systematic way to protect margins, bridge the ERP-MES gap, and systematically reduce manufacturing waste through data-driven control.
The Real Cost of High-Tolerance Scrap in Discrete Manufacturing
Margin erosion in discrete manufacturing rarely stems from a single catastrophic failure. Instead, it accumulates through recurring scrap on tight-tolerance runs where estimate-versus-actual job costing reveals severe margin leakage. When a CNC machine or stamping press produces out-of-spec parts, the financial impact extends far beyond the wasted raw material. Machine time is lost, downstream assembly schedules slip, and OTIF metrics degrade as expedited replacement runs disrupt the plant floor.
Plant managers typically respond to chronic scrap by adjusting feeds, speeds, or offsets manually based on shift handoffs and operator intuition. This approach introduces high variance between shifts. One operator's adjustments might stabilize a process temporarily, while the next shift sees the same machine drift back out of tolerance. Siloed ERP and MES data compounds the issue, leaving engineering teams without a unified view of how raw material heat numbers correlate with final inspection failures.
Algorithmic parameter tuning uses machine learning to analyze historical and real-time sensor data, automatically adjusting manufacturing variables to maintain tight tolerances and minimize scrap.
Strategy 1: Dynamic Feed-Rate and Spindle Speed Optimization
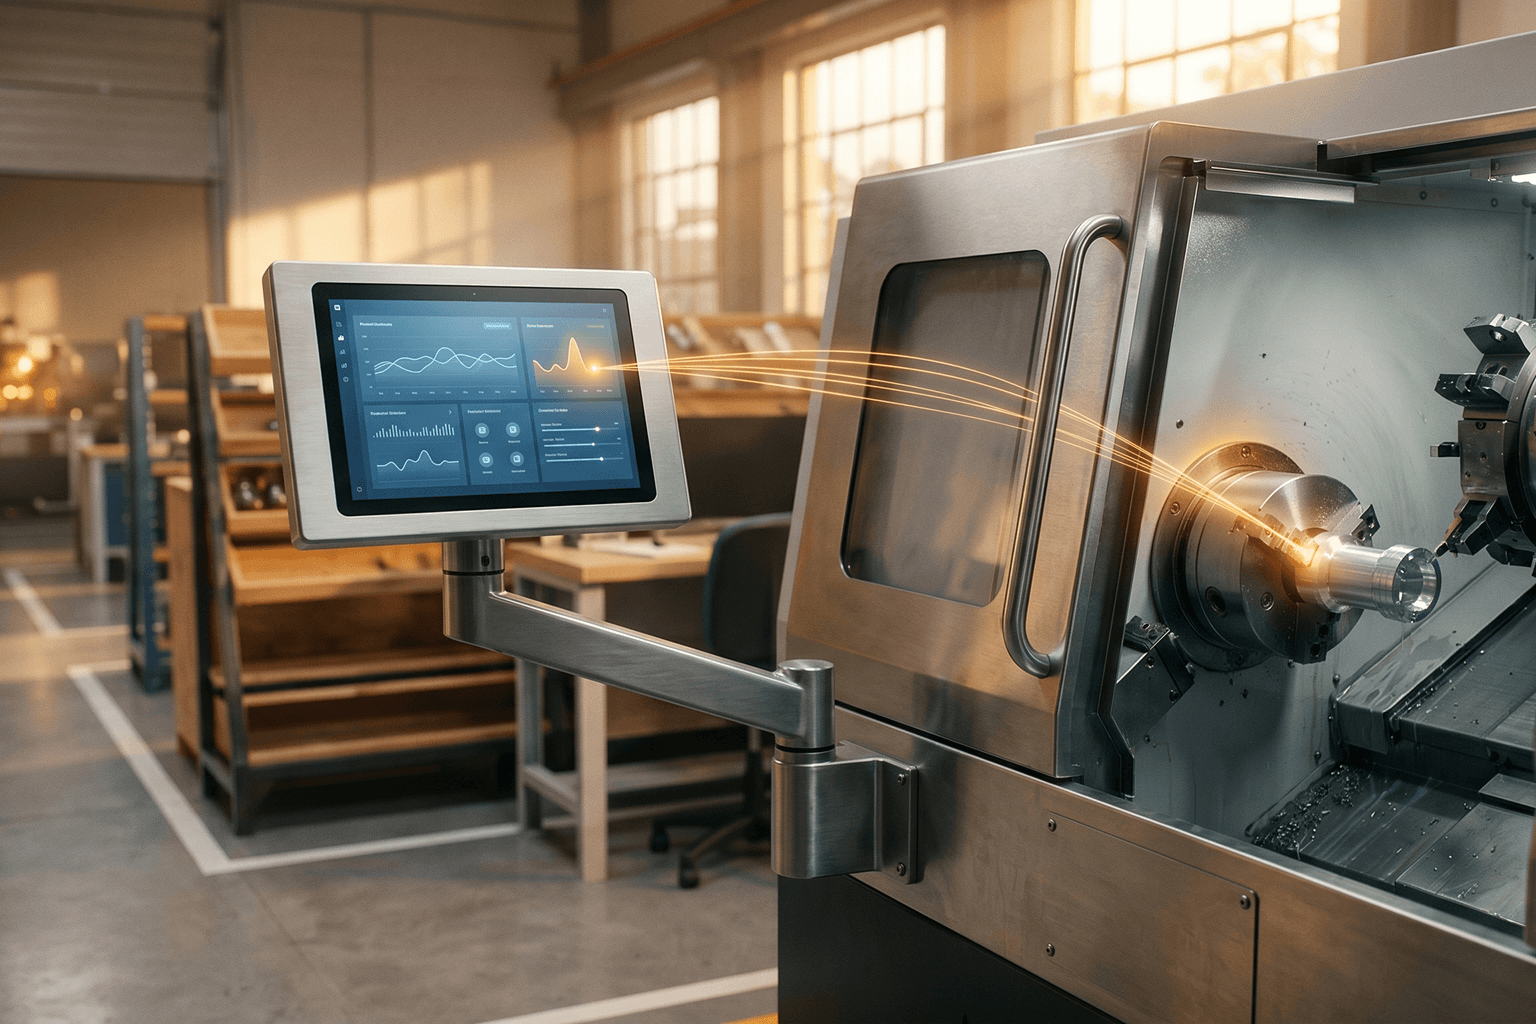
Static CNC programs are engineered for worst-case material scenarios, meaning machines spend the majority of their lifecycle running at sub-optimal parameters. Dynamic feed-rate and spindle speed optimization replaces static G-code programs with algorithms that adjust cutting parameters in real-time based on actual load sensors and vibration feedback.
As a cutting tool wears or encounters harder inclusions in the raw stock, the model adjusts feed rates milliseconds before the deflection causes dimensional error. This continuous micro-adjustment protects the workpiece from surface tearing and prevents premature tool breakage. For plants dealing with expensive exotic alloys or tight aerospace tolerances, this strategy stabilizes the cutting zone and directly lowers scrap rates without sacrificing cycle time.
Strategy 2: Historical Batch Data Clustering for Error Prevention
Most plants sit on years of untapped historical data buried across disparate ERP job histories and MES inspection logs. Historical batch data clustering applies unsupervised machine learning algorithms to mine this operational archive, isolating the hidden multivariate correlations that drive out-of-spec parts.
By clustering past runs by material lot, ambient humidity, machine ID, and tooling batch, engineers can identify the exact precursor conditions that preceded past scrap events. These insights transform reactive troubleshooting into proactive prevention. Instead of investigating a failure after the parts hit the CMM table, the plant can flag high-risk batches before the job is even loaded onto the spindle.
Strategy 3: Closed-Loop CMM Feedback Integration
Coordinate Measuring Machines (CMM) often operate as quality gates at the end of the line, catching bad parts after they have already been produced and consuming valuable inspection labor. Closed-loop CMM feedback integration closes the loop between quality control and machining by feeding inspection data directly back into the parameter optimization algorithm.
When the CMM detects a dimensional trend leaning toward the upper or lower specification limit, the system calculates the required offset adjustment and pushes it directly to the CNC controller automatically. This eliminates the delay between manual inspection reporting and machine compensation. Tolerances stay centered within the specification band, keeping scrap rates near zero during long production runs.
Strategy 4: Thermal Drift Compensation Modeling
Machine tool geometry changes constantly throughout the day as spindles warm up, coolant temperatures fluctuate, and ambient shop floor temperatures shift from morning to afternoon. Thermal drift compensation modeling uses predictive regression algorithms to account for these temperature-induced dimensional changes before they impact part quality.
By placing temperature sensors at critical structural nodes across the machine frame and spindle housing, the algorithm learns the specific thermal expansion profile of each asset. It then applies real-time coordinate transformations to compensate for expansion and contraction. This ensures that the first part off the machine on a cold Monday morning hits the exact same tolerance as the hundredth part produced at the end of the shift.
Strategy 5: Operator-in-the-Loop Active Learning Workflows
Advanced algorithms fail on the shop floor if operators do not trust their recommendations or understand why a parameter change was suggested. Operator-in-the-loop active learning bridges the gap between data science and plant floor reality by treating shop-floor tribal knowledge as a critical data input.
When the algorithm suggests a parameter adjustment, the interface prompts the machinist to validate or override the recommendation based on physical observations, such as chip color or unusual acoustic feedback. The system then logs this operator feedback to retrain and refine its underlying models. This collaborative workflow builds institutional trust, accelerates user adoption, and ensures that algorithmic tuning reflects physical shop-floor realities.
Moving Past the Failed Pilot: Implementation Roadmap
Many manufacturing operations struggle to move AI initiatives past a single standalone pilot because projects lack integration with core plant systems or take too long to show financial return. Deploying a production-ready parameter tuning model requires a structured, phased approach that connects directly to existing OT and IT infrastructure without requiring a costly software overhaul.
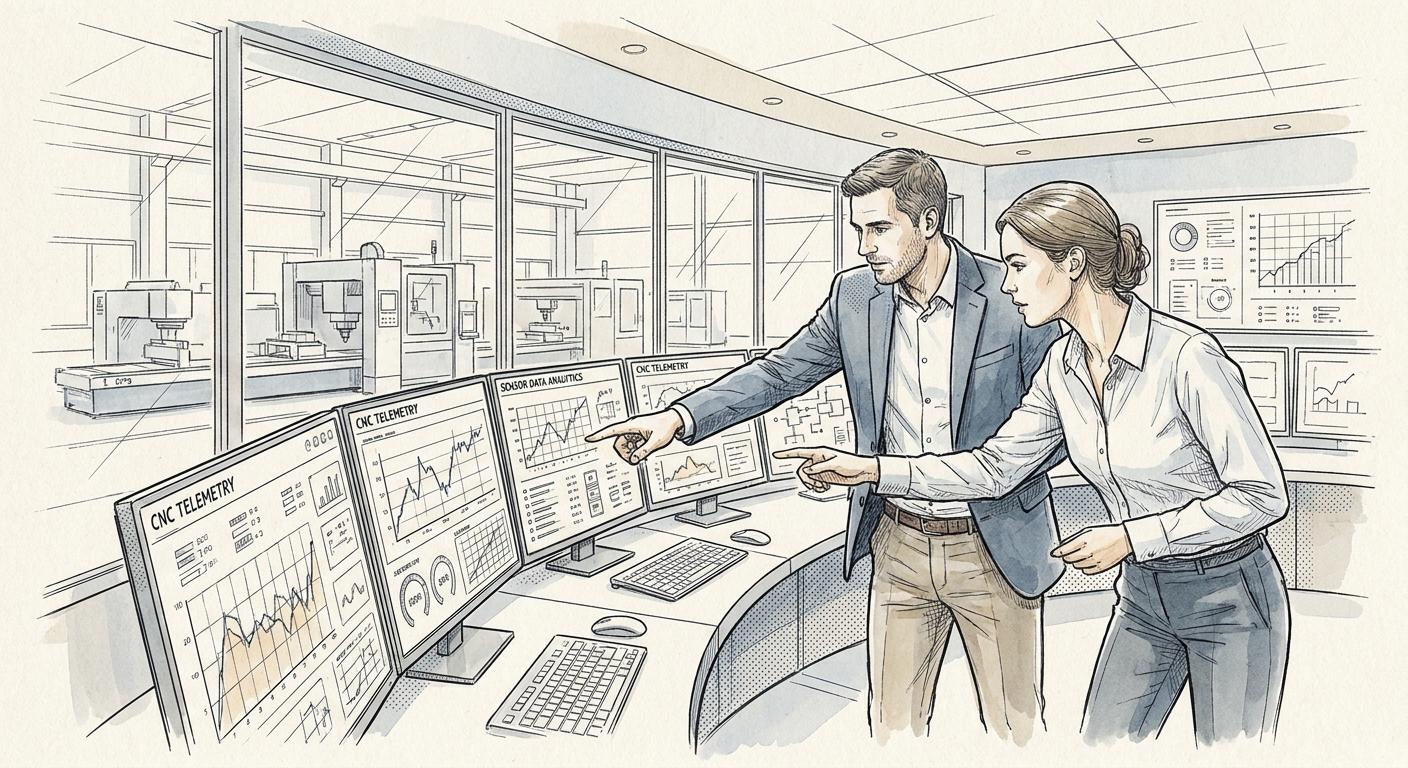
Organizations can achieve first measurable results within a 60-90 day window by focusing on a single high-scrap constraint asset rather than attempting an enterprise-wide rollout. By integrating machine telemetry, historical MES logs, and quality data into a unified workflow, operations teams can stabilize tight-tolerance production, protect margins, and build a repeatable playbook for continuous manufacturing waste reduction.
Frequently Asked Questions
What is algorithmic parameter tuning in manufacturing?
Algorithmic parameter tuning uses machine learning models to dynamically adjust machine settings like feed rate, speed, and depth of cut in real-time to optimize output quality and minimize waste.
How quickly can parameter tuning models show ROI in a plant?
Production-ready parameter tuning models can deliver measurable results and reduction in scrap rates within a 60 to 90 day implementation window.
Do we need to replace our existing MES or ERP to use AI parameter tuning?
No, parameter tuning solutions integrate directly with existing OT sensors and IT infrastructure rather than requiring a rip-and-replace software overhaul.
Book a Manufacturing Diagnostic at ifor.ai/solutions/manufacturing

Ofer Hermoni, Ph.D.
Founder & Chief AI Officer at iForAI